Skip To Content

7 Tips for Choosing Custom Aluminum Tri Fold Blind Rivets

Choosing the right Custom Aluminum Tri-Fold Blind Rivets begins with the joint, not the catalog photo. These rivets can form a broad blind-side footprint, helping secure thin or brittle materials when access is available from one side. But a promising shape does not guarantee a reliable assembly. Grip range, hole size, panel thickness, rivet-body material, and installation-tool compatibility all matter. A rivet that is too short may not form correctly; one that is too long may loosen or distort the workpiece. Small details matter.

This guide presents seven practical checks for comparing options, from material compatibility to sample testing. For transparency, the following specialist and quotation are illustrative, not a verified real-world attribution: fictional fastener engineer Elena Ward says, “Choose for the joint you have, then verify the set rivet in the actual materials.” That is a useful discipline, not a substitute for testing. Check the manufacturer’s specifications, install samples with the intended tool, and inspect the formed backside for consistent expansion and secure clamping. A clean-looking head can still hide a poor joint. One limitation deserves attention: application conditions vary, so no single rivet choice suits every assembly. The aim is a reasoned shortlist, supported by measurements and hands-on checks, rather than confidence based on appearance alone.
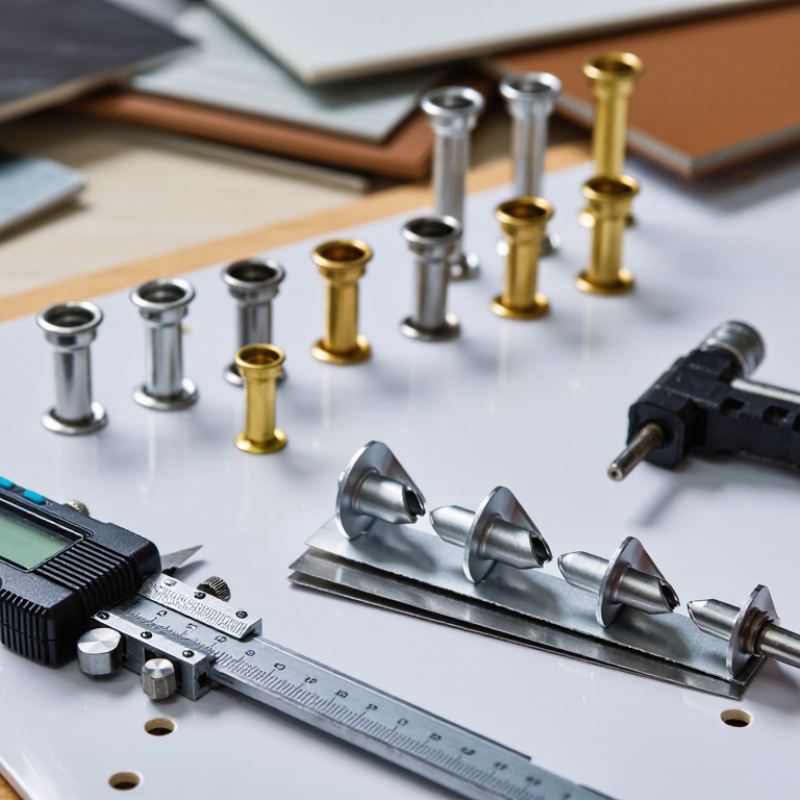
7 Tips for Choosing Custom Aluminum Tri Fold Blind Rivets

Understanding the Design of Custom Aluminum Tri-Fold Blind Rivets

A custom aluminum tri-fold blind rivet is designed around how its body opens behind the workpiece. During setting, the mandrel expands the rivet body into three broad legs. These legs spread the clamping load across the blind side, which can help when access is limited or the material is relatively soft. They still need a sound surface to bear against.

Fit starts with the grip range: the combined thickness of the joined parts must sit within the rivet’s rated range. Hole diameter matters too. An oversized hole can reduce grip, while a tight hole may prevent clean setting. Specify head style, body alloy, mandrel material, and any coating for the service environment.

Small details matter. In damp or salty conditions, dissimilar metals can increase corrosion risk; test the complete joint, not just the rivet. The International Aluminium Institute reports that recycled aluminium requires about 5% of the energy used for primary aluminium production. That supports aluminium’s material-efficiency case, but it does not prove joint strength or durability. I would treat it as context, then validate the custom rivet with setting trials and load tests on the actual materials.

Assessing Material Compatibility and Joint Requirements

Start with the sheet alloy and temper, then match the rivet body and mandrel to the joint. ASTM B209/B209M-21a lists minimum tensile strengths of about 215 MPa for 5052-H32 sheet and 290 MPa for 6061-T6 sheet, subject to product form and thickness. These figures describe the sheet, not the finished joint’s allowable load. A stronger sheet does not automatically make a safer fastening choice. Fit matters.

Next, confirm the combined material stack, hole size, and grip range. A tri-fold rivet opens into three legs, spreading bearing load across the blind side; that can help with thin or softer panels. But an oversized hole or a grip range mismatch can still cause loose joints, panel crushing, or incomplete setting. NASA’s Fastener Design Manual, Reference Publication 1228, discusses joint load paths and fastener selection; use its engineering principles alongside the rivet maker’s tested installation data. Check for dissimilar-metal contact, moisture, and coatings, especially where a mandrel remains in the assembly. Test the stack. I would not rely on a catalog pull-strength figure alone: make sample joints from the actual sheet thicknesses, inspect the folded legs, and test them under the expected load.

7 Tips for Choosing Custom Aluminum Tri Fold Blind Rivets - Assessing Material Compatibility and Joint Requirements
Tip What to Assess Practical Guidance Why It Matters
1. Match the rivet body to the joined materials Base metals, coatings, moisture exposure, and the possibility of galvanic corrosion. For aluminum-to-aluminum assemblies, an aluminum rivet body is often a compatible starting point. For dissimilar metals or outdoor service, check the material combination and use an appropriate protective finish or isolation method where needed. Electrical contact between dissimilar metals in a wet environment can accelerate corrosion. Compatibility depends on the specific metals, coatings, and service conditions.
2. Specify the mandrel material separately Whether the application permits a steel mandrel, or needs a mandrel material more compatible with the surrounding assembly. Do not assume an aluminum-body rivet has an aluminum mandrel. Confirm the mandrel material, whether it remains captive after setting, and whether its presence is acceptable for corrosion and electrical requirements. Rivet bodies and mandrels can be made from different materials, which may affect corrosion behavior and the suitability of the finished joint.
3. Measure the total grip thickness The combined thickness of every layer being fastened, including coatings or compressible layers that affect the joint. Select a rivet whose published grip range includes the measured stack thickness. If the stack varies, check that the full expected range is covered rather than sizing from a nominal thickness alone. A rivet outside its grip range may not form the intended blind-side legs or clamp the layers reliably.
4. Confirm the hole and access conditions Hole diameter, hole quality, tool access, and the available space behind the workpiece. Use the hole diameter and installation instructions specified for the selected rivet. Verify that the blind side has enough room for the tri-fold legs to open without striking nearby parts. An unsuitable hole or obstructed blind side can prevent proper setting and reduce joint consistency.
5. Check whether a tri-fold head is suitable for the sheet Sheet hardness, brittleness, surface condition, and the need to spread load over a wider area. Tri-fold rivets form three legs on the blind side and can distribute bearing load over a broader area than a conventional blind-rivet tail. Confirm that the intended head style provides adequate support on the accessible side. The folding legs can be useful with softer or more fragile materials, but they do not eliminate the need to check sheet deformation and surface damage.
6. Size the joint for actual loads Shear and tensile loads, vibration, impact, number of fasteners, edge distance, and load direction. Use published strength data for the exact rivet size, material, and grip range. Design the joint around the weaker of the rivet and joined materials, and test representative assemblies when loads are safety-critical. Strength values vary by rivet design and test conditions; a generic capacity cannot reliably represent every custom configuration.
7. Validate installation and service conditions Setting-tool compatibility, installation repeatability, temperature, chemicals, and long-term exposure. Confirm that the tool can set the specified rivet and that the installed head and formed legs meet the application requirements. Test samples using the actual materials, hole preparation, coatings, and service environment. Installation quality and environmental exposure affect joint performance, so a sample build helps verify the complete assembly rather than the rivet alone.

Selecting Rivet Size, Grip Range, and Head Style

Begin with the full thickness of the joined sheets, including paint or a gasket. Choose a grip range that contains that measurement, not one that barely reaches it. Too short, and the blind-side legs may not form properly. Too long, and the joint can feel loose. Measure twice. Check the specified hole diameter and drill a clean, round hole; an oversized hole can let the rivet shift. Match rivet diameter to the load and material thickness, then verify the joint with a sample assembly.

A tri-fold rivet spreads its legs behind the panel, creating a broad bearing area. That can help when fastening thin or softer sheet, but it does not replace a load check. NASA’s Fastener Design Manual, RP-1228, discusses evaluating fastener loads and joint design; use the assembly’s actual shear and pull-through requirements rather than choosing by appearance. The Aluminum Association lists aluminum’s density at about 2.7 g/cm³, a useful reminder that lightweight panels can still need careful support around the hole.

Choose a head style to suit the surface and bearing needs. A dome head offers a broad visible seat; a low-profile head may reduce snagging. Countersunk heads need a correctly prepared recess and enough sheet thickness. Small detail. Also check clearance behind the panel for the folded legs, and consider corrosion compatibility between the rivet and sheet metals. I still test a few samples in the real stack-up; nominal dimensions do not always capture coatings, burrs, or a slightly uneven surface.

Evaluating Load Capacity and Environmental Conditions

Choosing an aluminum tri-fold blind rivet starts with the joint, not the catalog. Identify the materials, combined thickness, and direction of force. A panel that pulls outward loads a fastener differently from one carrying a sideways shear load. Check both tensile and shear ratings, then leave a sensible margin for vibration, handling, and uneven load sharing. Do not treat a published maximum as a routine working load. Small details matter.

Measure the grip range across the actual stack-up, including paint, sealant, or a soft gasket. Too short, and the legs may not fold fully; too long, and the head may sit loose. For thin sheet, inspect the formed blind side and surrounding material after a sample installation. A tidy head can hide a weak joint. Use a few test pieces. It is worth checking.

Environmental conditions change the choice. Moisture, road salt, cleaning chemicals, and trapped water around a lap joint can accelerate corrosion. Aluminum rivets may be a poor match with certain dissimilar metals, so confirm compatibility and coating guidance in the supplier’s technical data. Check operating temperature and exposure cycles, not just indoor test values. Designers sometimes focus too heavily on pull strength. I would revisit that assumption when an assembly faces weather or repeated movement. A small test using the real material stack can reveal problems early, though it cannot replace verified ratings.

Verifying Installation Tools and Quality Specifications

Before ordering custom aluminum tri-fold blind rivets, confirm the setting tool matches the rivet’s diameter and grip range. Check its nosepiece, pulling stroke, and capacity against the supplier’s installation data. A tool that bottoms out too early may leave the folded legs uneven behind the sheet. Fit matters. Test several samples on material matching the real panel, not just a loose coupon. Record mandrel break-off, head seating, and any panel distortion. A clean-looking head can still hide a weak set.

Ask for lot-specific dimensions and mechanical test results, including tensile and shear strength. ISO 14589:2000 defines mechanical testing for blind rivets, including tensile and shear tests; use its methods when reviewing supporting data. Compare results with the drawing and application requirements, rather than applying one strength value to every rivet size. Verify body diameter, grip range, head dimensions, and mandrel retention. Keep the inspection method consistent between incoming lots. One awkward detail: tool settings can drift as nosepieces wear, so a passing sample today is not proof of stable production next month. Recheck settings at changeovers and retain a few installed samples for comparison.

7 Tips for Choosing Custom Aluminum Tri-Fold Blind Rivets

Suggested selection-priority allocation for planning a rivet review. These percentages are illustrative, not measured test results or product specifications.

Start by matching the rivet’s grip range to the total material thickness, then confirm the hole size and tool compatibility. Verify setting performance and blind-side formation on representative samples, and check material compatibility, corrosion requirements, and applicable quality documentation before production.